Reorder point equals expected usage during lead time plus safety stock, and the trigger is simple: place a new order the moment on-hand inventory drops to that number. The formula sounds basic, but getting the inputs right determines whether parts show up on time or a line sits idle. Below, we walk through the math with worked examples you can apply directly to your own parts list.
TL;DR:
- Use 6 to 12 months of history for average usage, and track lead time from purchase order until stock is ready after inspection.
- Use a days of supply buffer for stable parts, but calculate statistical safety stock for critical spares only when usage history supports reliable variance estimates.
- Target 90% to 95% service for routine consumables; exceed 95% for safety or compliance parts and single points of failure, accepting higher carrying costs.
- Pilot calculations on 50 to 100 SKUs for 4 to 6 weeks, then adjust buffers using stockouts and carrying costs before expanding across the plant.
- Recalculate immediately after a supplier change or usage shift, and keep minimum order quantities separate from the reorder trigger, which determines when to buy.
Table of Contents
- What reorder point means and how the formula works
- How to calculate average usage, lead time, and safety stock
- Two worked examples: steady part and critical spare
- Choosing safety stock and service levels for parts
- Adjusting reorder points for real-world uncertainty
- Putting reorder points into daily operations
- How a CMMS keeps reorder points accurate over time
- A practical view on reorder points and uptime
- Put parts reorder points on autopilot with MPulse
- FAQ
- Sources
What reorder point means and how the formula works
The reorder point (ROP) is the inventory level that triggers a new purchase order before stock runs out. It accounts for how much you consume while waiting for a replacement shipment, plus a cushion for the unexpected. Wikipedia’s reorder point entry defines it as expected consumption during replenishment lead time plus safety stock, expressed in two common forms.
The basic deterministic formula works when usage and lead time barely change:
- ROP = average daily usage × lead time (in days)
- ROP = lead-time demand + safety stock (the more general version, used whenever demand or supply timing varies)
For parts with unpredictable demand, planners add a service-level term using a z-score, which converts a target confidence level (say, 95%) into a statistical multiplier applied to combined demand and lead-time variability. This expanded formula appears in the same Wikipedia reference and underlies most CMMS and ERP reorder calculations.
A few terms worth fixing before you calculate anything:
- Lead-time demand: the quantity you expect to use between placing an order and receiving it.
- Safety stock: extra inventory held to absorb demand spikes or shipment delays.
- Service level: the probability you will not run out of stock during a replenishment cycle.
Keep units consistent. If lead time is measured in days, usage must be daily. Mixing weekly usage with a lead time in days is the single most common setup error we see in parts inventories.
How to calculate average usage, lead time, and safety stock
Three inputs drive every reorder point calculation, and each deserves its own discipline.
- Average usage rate: Pull 6 to 12 months of consumption history for the part, then calculate a daily or weekly average. Shorter windows react faster to real shifts but amplify noise from one-off repairs or seasonal spikes.
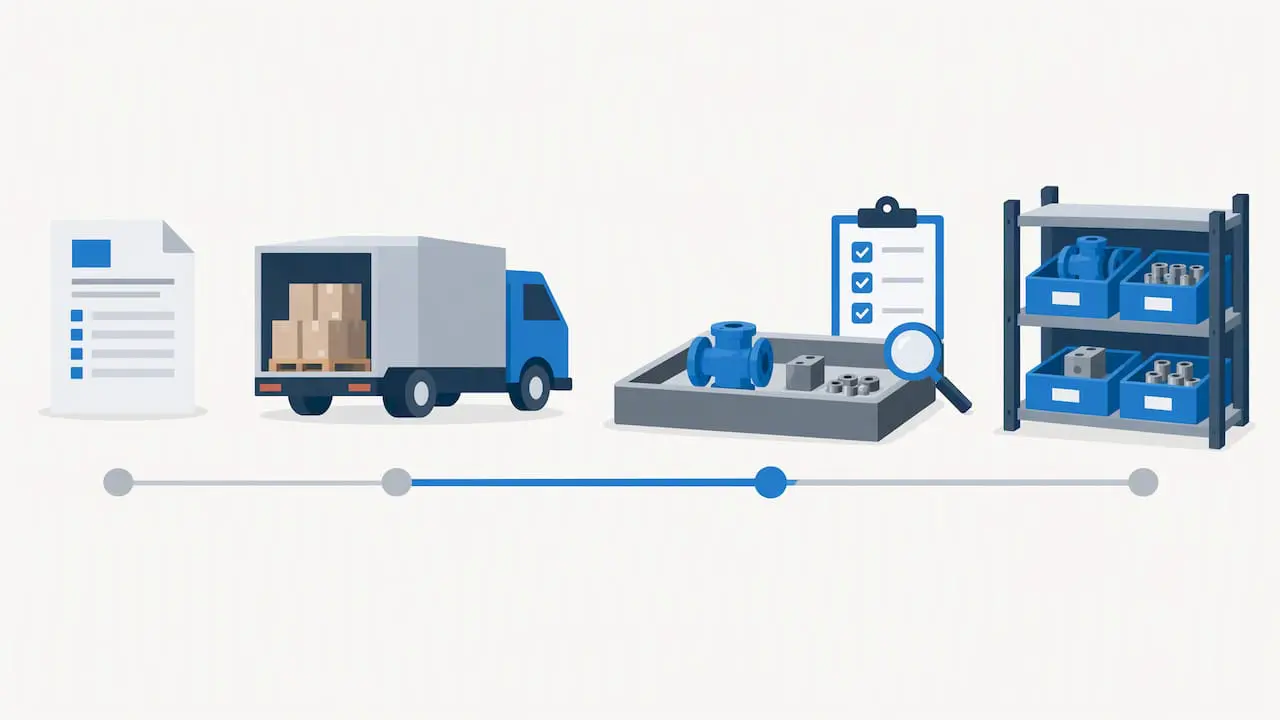
- Lead time: Track the actual time between placing a purchase order and receiving usable stock, not the supplier’s quoted time. Internal lead time (requisition approval, receiving, inspection) belongs in this number too.
- Safety stock: Choose a method that matches your data quality. A days-of-supply buffer (for example, five extra days of average usage) works for stable, low-value parts. A statistical service-level method works better for critical spares with enough history to compute a standard deviation. When data is sparse, a simple heuristic such as “one extra unit per critical asset” can hold until enough history accumulates.
The AccountingTools reorder level formula notes that the simple average-usage calculation often understates risk when demand is volatile. Its suggested fix swaps in maximum daily usage instead of the average, or adds an explicit safety stock term: (Max daily usage × Lead time) + Safety stock.
Pro Tip: Record lead time from purchase order date to shelf-ready date, not just delivery date; receiving and inspection delays quietly extend real lead time by days.
Two worked examples: steady part and critical spare
Numbers make the formula concrete. Here are two parts with very different risk profiles.
- Steady-demand MRO part (lubricant cartridges): Average usage is 4 units per day, lead time is 10 days, and the team wants a 2-day safety buffer. Lead-time demand is 4 × 10 = 40 units. Safety stock is 4 × 2 = 8 units. Reorder point = 40 + 8 = the calculated sum of units based on usage and buffer. Order triggers the moment on-hand stock hits 48.
- Critical sporadic spare (pump seal kit): Average demand is 0.5 units per week with a standard deviation of 0.8, and lead time averages 3 weeks with a standard deviation of 1 week. For a 95% service level, the z-score is approximately 1.65, per the statistical approach described on Wikipedia. Combined demand and lead-time variability produces a safety stock calculation that typically lands around 2 to 3 units for a part this volatile, bringing the reorder point to roughly 4 to 5 units depending on the exact variance formula applied.
A small change in lead time swings the number more than you’d expect. If the pump seal kit’s lead time stretches from 3 weeks to 5 weeks because of a supplier delay, lead-time demand alone rises from 1.5 units to 2.5 units, before any safety stock adjustment. That sensitivity is why the Springer study on high-tech manufacturing at ASML treats demand uncertainty and lead-time uncertainty as separate problems rather than folding both into one generic buffer.
Run both calculations for your own top parts before trusting any default safety stock percentage pulled from a spreadsheet template.
Choosing safety stock and service levels for parts
Safety stock decisions come down to a tradeoff between stockout risk and carrying cost, and the right target depends on what the part protects.
- Cycle service level measures the probability of not stocking out during a single replenishment cycle; it is the easier number to compute and the one most z-score formulas use.
- Fill rate measures the percentage of demand met directly from stock across all cycles; it is a better fit for parts with frequent, small withdrawals.
- For routine MRO consumables, a service level in the 90 to 95% range is typically sufficient. For parts tied to safety, compliance, or single points of failure, many operations push past 95%, accepting higher holding cost in exchange for lower downtime risk.
The statistical safety stock formula multiplies a z-score (tied to your target service level) by the combined standard deviation of demand and lead time. The ASML case study found that separating hedging tactics at the master-schedule level from safety stock at the component level improved service outcomes, though it also raised total inventory investment, a tradeoff worth naming rather than hiding.
When you lack enough history to compute a reliable standard deviation, a heuristic (days-of-supply multiplied by a risk factor) is a reasonable placeholder until a pilot generates better data.
Pro Tip: Start new or rarely used spares at a conservative heuristic safety stock, then recalculate with real variance data after the first few actual usage events.
Adjusting reorder points for real-world uncertainty
Formulas assume stable conditions that rarely hold for long. A few adjustments keep ROP accurate as conditions shift.
- Lead-time variability belongs inside the safety stock term, not as a separate buffer bolted on afterward; treating demand variance and lead-time variance as one combined statistic, as the ASML research recommends, avoids double-counting risk.
- Minimum order quantities (MOQs) from suppliers can push your actual order size above the mathematically optimal EOQ, which means your ROP trigger still fires at the calculated point, but the order quantity itself is constrained by what the supplier will ship.
- Pooling and lateral transshipments, sharing spares across sites or pulling from a sister facility, often reduce the need for oversized safety stock better than simply raising the buffer at every location.
- Emergency shipment procedures matter most for rarely used or newly introduced parts. The SSRN research on robust spare parts management found that adaptive policies combining emergency shipments with lighter statistical assumptions outperformed relying on historical averages alone when data is scarce.
For parts under active condition monitoring, the Condition-Based Service Level approach ties ordering timing to actual asset condition rather than fixed calendar-based triggers, which suits expensive, highly reliable spares with long lead times.
Putting reorder points into daily operations
A formula only helps if it runs on current data and gets reviewed on a schedule.
- Build a data checklist: usage history by part, logged lead times (order date to shelf-ready date), current on-hand and on-order quantities, and supplier reliability notes. Flag any part missing more than one of these inputs before trusting its ROP.
- Run a pilot before a full rollout: apply the formulas to a set of 50 to 100 SKUs for 4 to 6 weeks, watching for stockouts and excess carrying cost, then adjust safety stock assumptions before extending the approach plant-wide. Our guidance on piloting MRO min/max levels walks through this process in more detail.
- Set a review cadence: assign ownership of ROP updates to a specific role, and trigger a recalculation whenever a supplier changes lead time, a part’s usage pattern shifts, or a stockout occurs.
Track stockout frequency, carrying cost per SKU, and order-to-receipt lead time as your core KPIs.
Pro Tip: Recheck reorder points immediately after any supplier switch, not on the next scheduled review, since lead-time assumptions often become outdated overnight.
How a CMMS keeps reorder points accurate over time
Spreadsheets handle the math, but they rarely catch the moment stock crosses a threshold or keep lead-time logs current without manual entry. A CMMS built for parts tracking closes that gap.
- Automated reorder alerts fire the moment on-hand quantity hits the calculated ROP, removing the manual check.
- Usage and lead-time history accumulate automatically from work orders and purchase receipts, which keeps the inputs behind your formula current.
- Purchase requisition workflows connect the reorder trigger directly to an approval chain, cutting the internal lead time that often gets left out of ROP math.
Our inventory features in MPulse CMMS support this cycle, and our guidance on inventory reordering covers how to connect min/max levels to purchase requisitions without manual spreadsheet updates.
A practical view on reorder points and uptime
Reorder point math is only as good as the discipline behind it. The formula takes minutes to compute; the real work is logging accurate lead times and revisiting assumptions after every supplier hiccup. Treat ROP as a living number tied to your maintenance records, not a one-time spreadsheet exercise, and it will protect uptime far more reliably than a static safety stock guess ever does.
— Mark
Put parts reorder points on autopilot with MPulse
Running the formulas above by hand works for a handful of parts, but most operations manage hundreds of SKUs across multiple storerooms, and that is where manual tracking breaks down. A CMMS tracks usage history and lead times automatically, then triggers purchase requisitions the moment a part hits its calculated reorder point, so nobody has to watch a spreadsheet.
- Automated reorder alerts remove the manual stock-check step entirely.
- Purchase requisition workflows route orders for approval without extra data entry.
- Add-ons like our Resource Planning Dashboard give visibility across every storeroom from one screen.
Review MPulse pricing plans, including Professional at $29 per month per user and Advanced at $79 per month per user, or look at our implementation and training services if you want support running your pilot.
FAQ
What is EOQ and ROP?
Economic order quantity (EOQ) is the order size that minimizes total ordering and holding cost, while reorder point (ROP) is the inventory level that triggers placing that order. ROP answers “when to order,” and EOQ answers “how much to order,” and the two work together in a standard replenishment system.
What is the 80/20 rule in inventory?
The ABC analysis rule holds that a small share of SKUs typically accounts for most inventory value or usage. In parts management, this means prioritizing tighter reorder point review and tracking for your highest-value or highest-use “A” items, while applying simpler heuristics to lower-priority “C” items.
What is the difference between safety stock and reorder point?
Safety stock is the buffer quantity held to protect against demand or lead-time variability, while the reorder point is the total trigger level, lead-time demand plus safety stock, at which a new order gets placed. Safety stock is one component inside the larger reorder point calculation, as described in the reorder point formula.
What is EOQ and formula?
EOQ is the order quantity that minimizes combined ordering and carrying costs, and it is typically calculated from annual demand, order cost, and holding cost per unit. It is used alongside the reorder point formula, with EOQ setting the order size and ROP setting the timing.
Sources
- Reorder point – Wikipedia
- Reorder level formula — AccountingTools
- Integrated production and safety stock planning in high-tech manufacturing: a comparative study at ASML